Factory Direct Solid Maple Hardwood Sports Flooring Company
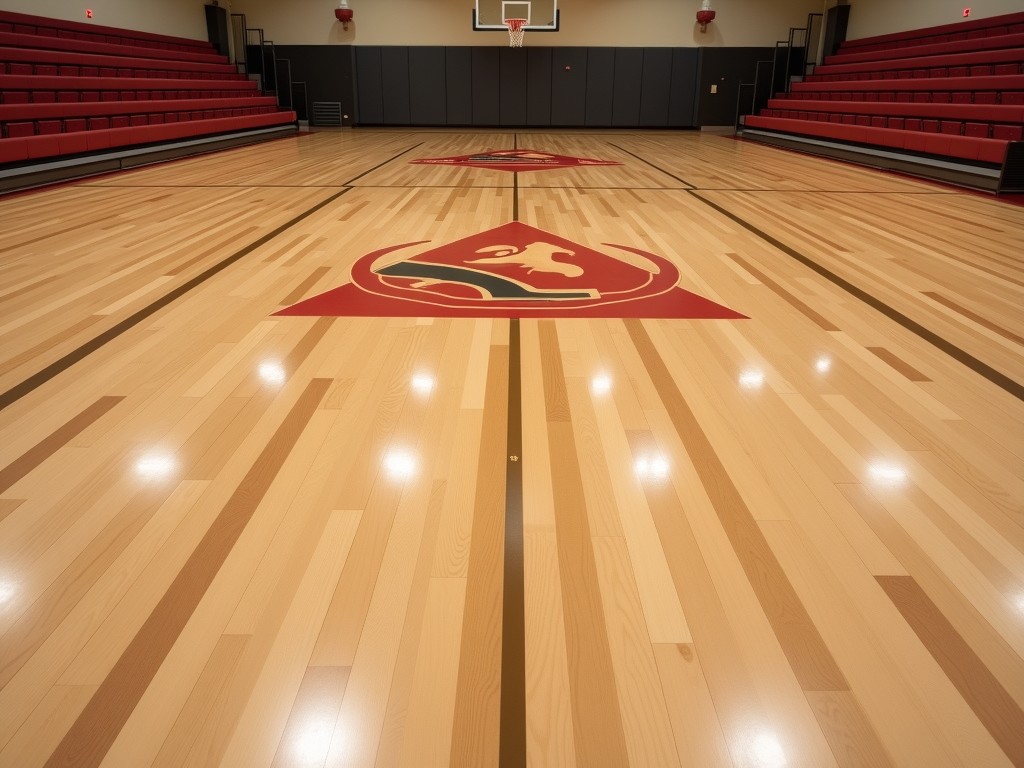
Factory Direct Solid Maple Hardwood Sports Flooring Company
Factory Direct Solid Maple Hardwood Sports Flooring
Product Overview
Solid maple is harvested from temperate forests and sawn to exact thicknesses for sports flooring. The wood’s cellular structure provides a homogeneous matrix that yields uniform stiffness and density across each board. This foundation supports predictable performance under repetitive impact loads.
Material Composition and Properties
Maple exhibits a specific gravity of approximately 0.70 – 0.75, translating to a density of 700‑750 kg/m³ when dried to 8 % moisture content. The Janka hardness rating averages 1 450 lbf, indicating resistance to surface indentation from equipment and foot traffic.
Dimensional stability is achieved through controlled kiln‑drying, limiting tangential shrinkage to under 0.2 % per percent moisture change. This reduces the likelihood of gapping or cupping in environments with fluctuating humidity.
Performance Characteristics
Sports flooring requires a balanced combination of shock absorption and surface friction to protect athletes while enabling precise movement. Solid maple systems typically achieve a shock absorption value of 25‑35 % when measured according to ASTM F2772, depending on underlayment thickness.
The static coefficient of friction for a finished maple surface ranges from 0.60 to 0.80, providing sufficient grip for lateral cuts without excessive resistance that could impede sprinting. Vertical deformation under a 1 500 N load generally stays below 2.0 mm, meeting the requirements for basketball and volleyball play.
Installation Considerations
A stable, level subfloor is essential; concrete slabs should meet a maximum deviation of 3 mm over a 2 m straightedge. A moisture barrier is installed when the slab’s relative humidity exceeds 75 % to prevent moisture migration into the wood.
Boards are typically fastened using cleat nails or staples at 150‑mm intervals along the tongue, allowing for natural expansion. Expansion gaps of 10‑12 mm are left at perimeter walls and fixed objects, concealed by base molding.
When adhesive installation is preferred, a polyurethane‑based adhesive with a flexible cure is applied to the subfloor, followed by a rolling process to ensure full contact and eliminate voids.
Maintenance and Service Life
Routine maintenance involves dry dust removal followed by a damp mop with a pH‑neutral cleaner. Periodic deep cleaning uses a low‑speed rotary machine with a non‑abrasive pad to restore surface texture.
The wear layer can be sanded and refinished up to three times over the floor’s life, depending on the initial thickness. A 22‑mm thick maple system commonly supports a service life of 25‑30 years in institutional sports facilities before requiring replacement.
Recoating with a commercial urethane finish every 3‑5 years maintains the coefficient of friction and protects against abrasion from shoe soles and equipment.
Typical Applications
Maple’s high hardness and consistent rebound make it suitable for sports that demand precise ball response, such as basketball and volleyball. The uniform surface minimizes variations in ball bounce that could affect gameplay.
- Indoor basketball courts – provides reliable ball bounce and player traction.
- Volleyball courts – offers adequate shock absorption for jump landings.
- Multi‑purpose gymnasiums – accommodates varied activities while maintaining performance standards.
- Training facilities – supports repetitive impact from agility drills and weightlifting.
These applications benefit from the material’s ability to retain performance characteristics after years of use, reducing the need for frequent surface interventions.
Customization Options
Thickness can be specified from 18 mm to 28 mm to match structural requirements and desired feel underfoot. Width options range from 70 mm to 105 mm, influencing the number of seams and visual appearance.
Lengths are typically random between 300 mm and 1 200 mm, but fixed lengths can be produced for specialized layouts. Edge profiles include square, eased, or micro‑beveled to accommodate different installation methods.
Surface finishes are available in water‑based urethane, oil‑based urethane, or penetrating oil systems, each offering distinct gloss levels and maintenance profiles. Custom staining is possible while preserving the wood’s natural grain.
Quality Assurance
Each board undergoes grading for knots, splits, and grain orientation, with allowable limits defined by industry standards. Moisture content is verified using calibrated meters before packaging to ensure uniformity across a batch.
Surface flatness is checked with a straightedge and feeler gauge, accepting deviations not exceeding 0.5 mm over a 300 mm span. Hardness spot tests confirm that the Janka value remains within the specified range.
Final inspection includes a visual assessment for finish consistency and adhesion, followed by a pack‑out procedure that protects edges and corners with corner boards and stretch film.
Technical Specifications
| Parameter | Typical Value | Notes |
|---|---|---|
| Density | 700‑750 kg/m³ | At 8 % MC |
| Janka Hardness | 1 450 lbf | Average for hard maple |
| Thickness Options | 18‑28 mm | Customizable per project |
| Width Options | 70‑105 mm | Nominal |
| Shock Absorption | 25‑35 % | ASTM F2772, depends on underlayment |
| Static Coefficient of Friction | 0.60‑0.80 | Finished surface |
| Vertical Deformation @ 1500 N | <2.0 mm | Meets sports‑floor standards |
| Moisture Content (MC) | 6‑9 % | Kiln‑dried, verified before shipment |
Frequently Asked Questions
Can dimensions be customized?
Yes. Thickness, width, and length can be adjusted to suit specific subfloor conditions and design preferences. Custom lengths are available for modular layouts.
What information is required before quotation?
Project area, desired thickness, finish type, and any special edge profiling. Subfloor condition and moisture readings help determine appropriate installation method.
How is quality inspected?
Each batch undergoes grading for visual defects, moisture content testing, hardness spot checks, and flatness verification before packaging.
What packaging methods are available?
Boards are bundled in moisture‑resistant wraps, placed on pallets with corner protectors, and secured with stretch film. Export packaging includes additional vapor barriers and corner boards.
What is the typical production lead time?
Lead time ranges from 3‑5 weeks for standard specifications, depending on order size and current schedule. Custom finishes or lengths may extend this period.
For further details, technical data sheets, or to request a project‑specific quotation, please contact our technical sales team.
Request a Quote